Blog

Why Choose Cast Iron Castings for Global Sourcing?

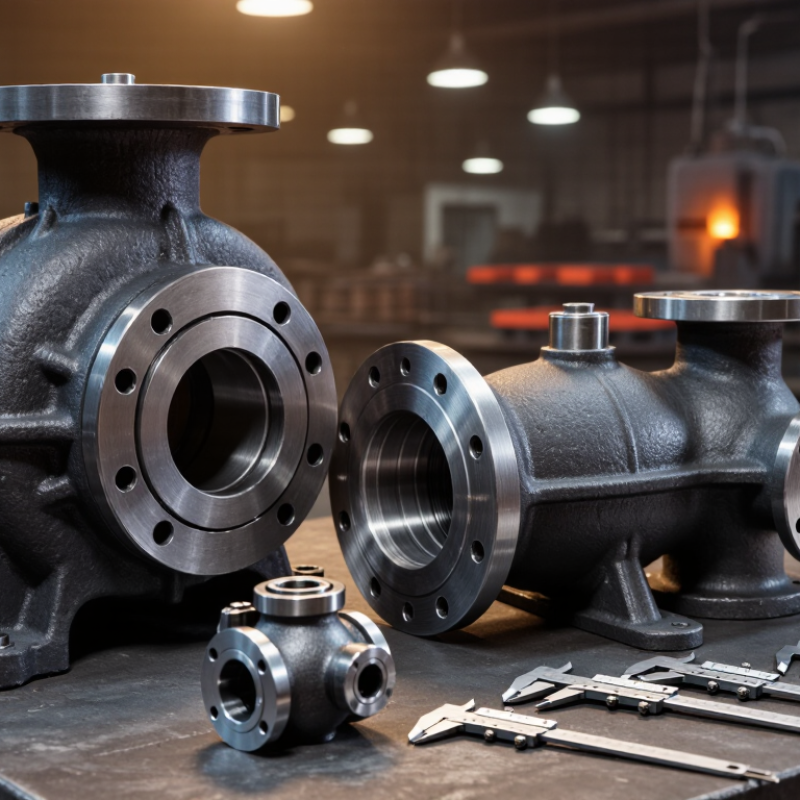
Global sourcing brings cost and capacity options, but distance makes quality harder to judge. Cast Iron Castings remain widely specified for pump housings, machine bases, valve bodies, and other components that need strength and dependable production. A well-made casting can combine useful wear resistance with shapes that might otherwise require multiple fabricated parts. That can simplify assembly. It is not automatic. Good drawings and process control matter as much as the material.

John Campbell, a respected casting researcher and author, has written: “The quality of a casting is determined by the quality of the liquid metal.” His observation points buyers toward foundry practice, not just quotations. For global buyers, practical checks include reviewing material specifications, sample parts, inspection records, and dimensional reports. Ask how the foundry controls melt chemistry, mold preparation, cooling, and finishing. A clean surface in a catalog photo proves little. Details matter. Where possible, compare a first article against the drawing and agree on acceptance criteria before volume orders begin.

A supplier’s capability, communication, and traceability may be as important as the unit price. The lowest quote can become expensive after rework, delayed shipments, or inconsistent batches. Yet cast iron is not right for every component; weight, corrosion exposure, and operating loads deserve scrutiny. That is a useful pause. Freight, tooling, and lead times also change the landed cost, sometimes more than buyers expect. A careful sourcing plan tests these assumptions early, then revisits them when production data arrives. No checklist removes every risk. But transparent specifications and steady quality reviews give teams firmer ground when selecting Cast Iron Castings across borders.
Why Choose Cast Iron Castings for Global Sourcing?

What Cast Iron Castings Are and How They Are Produced

Cast iron is an iron-carbon alloy shaped by pouring molten metal into a prepared mold. Its carbon content helps the metal flow into detailed cavities, then harden into a rigid component. Foundries commonly melt iron with carefully selected recycled or virgin materials. Operators monitor temperature and composition because small changes can affect strength, hardness, and machinability. The details matter. Before pouring, the mold is formed around a pattern, which creates the intended shape and allowances for shrinkage. Sand molds are widely used, though other mold systems suit particular production needs.

Molten iron enters the mold through channels designed to guide flow and reduce turbulence. Once the casting cools, workers remove the mold material, trim gates, and clean the surface. Some parts receive heat treatment or machining to meet dimensional requirements. Inspection may include visual checks, measurements, and testing suited to the part’s function. A rough surface is not automatically a defect, but cracks or dimensions outside specification need attention. The process is not perfectly tidy: mold design, cooling, and material control all involve trade-offs. For global sourcing, clear drawings and agreed inspection criteria help buyers and foundries discuss those trade-offs before production begins. No process eliminates every variation.

Material Properties That Make Cast Iron Suitable for Industry

Cast iron earns its place in industrial equipment through a useful mix of strength, damping, and castability. ASTM A48/A48M Class 30 gray iron specifies a minimum tensile strength of 30,000 psi. Its graphite flakes help dissipate vibration, which can matter in machine bases, pump housings, and gearboxes. Less chatter. That can support steadier operation, though mounting and operating conditions still matter.

Ductile iron offers a different balance. ASTM A536 Grade 65-45-12 specifies minimum tensile strength of 65,000 psi, yield strength of 45,000 psi, and elongation of 12%. These figures help engineers compare grades when parts face impact or repeated loading. They are specification values, not guarantees for every casting. Section thickness, cooling, and quality control affect the final part.

Cast iron also flows well into complex molds, allowing ribs, bosses, and mounting features to be formed in one component. That can reduce assembly work. Yet geometry alone does not ensure a sound casting; inspection and process control remain essential. Buyers should match the grade to the load, temperature, and machining needs, then confirm the supplier’s test records. A datasheet is useful, but real service conditions can still surprise.

Applications Commonly Served by Cast Iron Castings

Cast iron castings appear in equipment that needs stiffness, wear resistance, and reliable shape retention. In water and wastewater systems, they form valve bodies, pump housings, and access covers. These parts often face vibration, moisture, and repeated handling. A heavy casting can be useful here. It can also make installation harder.

Construction and agricultural machinery use cast iron housings, brackets, pulleys, and engine components. Gray iron dampens vibration, which can help reduce operating noise in machine bases and housings. Ductile iron offers greater toughness for parts exposed to impact or bending. The grade matters. Choosing by price alone can lead to a part that cracks, wears quickly, or weighs more than the design allows.

For global sourcing, application details should guide the specification. Buyers can share operating loads, temperature ranges, drawings, and machining requirements before requesting quotations. Ask how dimensional checks and material tests are documented. A casting may look sound but still need inspection for internal defects. One assumption deserves a second look: thicker walls do not automatically mean a longer service life. Poorly designed sections may cool unevenly and increase defect risk. The foundry and engineering team should review critical features together.

How to Evaluate Global Casting Suppliers

When evaluating global casting suppliers, start with the part, not the sales presentation. Share a controlled drawing, annual volume, critical dimensions, and service conditions. Ask whether the foundry regularly pours the required iron grade and casting weight. A heavy pump housing and a thin valve body need different process controls. Details matter. Request written tolerance capability, gating approach, and machining scope before comparing prices.

Review how the supplier manages patterns, melting records, inspection, and nonconforming parts. Ask for sample inspection reports and material certificates linked to a casting batch. A polished sample is useful, but it cannot show repeatability. Look for dimensional checks, hardness testing, and any required nondestructive examination. If a defect appears, ask who investigates it and how corrective actions are verified. Answers may be imperfect. A supplier that openly identifies a process limitation can be more credible than one promising zero defects.

Assess engineering response times across time zones, and confirm who controls drawing revisions. Clarify tooling ownership, sample approval, production lead time, and packaging for sea freight. Castings can arrive with rust, damaged edges, or unclear labels when protection and identification are vague. Request photos of packed goods and a lot-marking plan. Compare total landed cost, not just the quoted casting price. A small pilot order may reveal practical issues that a spreadsheet misses.

Why Choose Cast Iron Castings for Global Sourcing?

ASTM A48 gray iron classes are defined by minimum tensile strength. Use the required grade as one part of supplier evaluation, alongside casting capability, inspection records, and compliance with your drawing and specification.

Values are approximate MPa conversions of ASTM A48 class designations in ksi. Actual casting properties depend on factors such as section size and production conditions; confirm requirements and test results with the supplier.

Quality, Cost, and Logistics Factors in Global Sourcing

Global sourcing of cast iron castings works best when quality is measured before shipment, not assumed from a quotation. Ask for casting-grade chemistry, tensile results where relevant, and dimensional reports tied to the drawing revision. A first-article inspection can reveal shrinkage, porosity, or machining stock problems while changes remain manageable. Details matter. Still, inspection plans add time and cost, and no report replaces a clear agreement on acceptance limits.

Compare total landed cost, not just price per casting. Include pattern or tooling charges, machining, protective packaging, freight, duties, and the inventory needed to cover long replenishment cycles. Heavy castings can make ocean freight economical, but port delays and missed vessel connections can disrupt production. Specify lifting points, pallet strength, moisture protection, and packing dimensions before the order is released. A low unit price can still be a poor deal. Supplier visits or independent audits may help assess process control, yet travel and language differences can complicate follow-up. Build realistic lead-time buffers and keep a modest safety stock for critical parts; the right level depends on demand variability and the cost of a line stoppage. That balance is not always obvious.

Why Choose Cast Iron Castings for Global Sourcing? — Quality, Cost, and Logistics Factors

Sourcing factor Relevant facts What buyers should evaluate
Material options Gray iron contains flake-shaped graphite; ductile iron contains graphite nodules. Ductile iron generally offers greater tensile strength and ductility than gray iron, while properties depend on grade and section size. Specify the required material grade and applicable standard. Common specifications include ASTM A48 for gray iron, ASTM A536 for ductile iron, EN 1561 for gray iron, and EN 1563 for ductile iron.
Strength and service performance Cast iron properties vary by composition, casting process, heat treatment, and casting geometry. A material designation alone does not establish that every section of a casting will have identical properties. Review mechanical-property requirements, test-piece provisions, operating loads, and the supplier’s inspection plan. Request evidence that testing represents the specified material and production process.
Vibration damping Gray iron’s graphite-flake structure gives it useful vibration-damping characteristics compared with many steel grades. Consider gray iron for suitable machine bases, housings, and similar components where damping matters. Confirm that its strength and impact limitations are acceptable for the application.
Shape and design flexibility Casting can produce complex shapes, internal passages, and substantial sections. Depending on design and production volume, a casting may reduce the need to assemble multiple fabricated parts. Review draft, wall thickness transitions, cores, machining allowances, and likely shrinkage or distortion with the foundry before finalizing the design.
Machining and finished dimensions Machinability depends on the iron grade, microstructure, hardness, and cutting conditions. Cast surfaces and as-cast dimensions do not automatically meet precision-machined requirements. Identify datum surfaces, tolerances, surface-finish requirements, and which features will be machined. Agree on dimensional inspection methods for critical features.
Corrosion protection Ordinary unalloyed cast iron is not stainless steel and can corrode in wet or corrosive environments. Coatings and other protection can affect both performance and maintenance needs. Specify the service environment, coating system, coverage, and acceptance criteria. Include coating inspection and repair requirements where relevant.
Total landed cost Tooling, casting complexity, alloy or grade, order quantity, yield, machining, finishing, inspection, and freight all affect total cost. Cast iron is not automatically the lowest-cost choice for every design or order size. Compare quotations on the same technical scope, including tooling ownership, sampling, testing, packaging, shipping terms, and recurring production costs.
Quality assurance Useful controls can include material verification, mechanical testing, dimensional inspection, visual examination, and non-destructive testing when required by the design or purchase specification. Set acceptance criteria and inspection frequency in advance. Define required certificates, traceability, defect limits, corrective-action procedures, and approval of production samples.
Weight and freight Cast iron has a density of approximately 7.1–7.3 g/cm³, depending on composition and structure. Its weight can therefore be a significant factor in transport and handling. Calculate shipment weight and packaging dimensions from the actual casting and packing design. Confirm handling equipment, route constraints, and carrier limits for each shipment.
Packaging and transit protection Castings can be damaged by impact, abrasion, moisture, or poor restraint during transit. Thin sections and machined surfaces may need particular protection. Agree on secure blocking, separation between parts, protection for machined faces, moisture control where needed, and packaging suitable for the transport route and storage period.
Supplier and logistics planning International sourcing adds lead-time, customs documentation, transport coordination, and communication requirements. Tooling development and sample approval can extend the initial schedule. Confirm production capacity, sample and approval milestones, export documentation responsibilities, shipping terms, contingency lead time, and a clear process for handling changes.

By continuing to use the site, you agree to the use of cookies. more information

The cookie settings on this website are set to "allow cookies" to give you the best browsing experience possible. If you continue to use this website without changing your cookie settings or you click "Accept" below then you are consenting to this.

Close