Top 10 Ancoo Rice Color Sorter Manufacturers Worldwide
Choosing a reliable rice color sorter requires more than comparing glossy brochures. In real milling plants, performance appears under pressure: dusty air, uneven grain flow, broken kernels, and long production shifts. The Ancoo Rice Color Sorter is often considered alongside other international solutions because rice processors need stable detection, accurate rejection, and manageable maintenance.
This guide introduces ten leading manufacturers worldwide. It examines their sorting technologies, camera systems, ejector response, processing capacity, energy use, and after-sales support. Practical factors matter. A machine may show excellent laboratory results yet perform differently when rice contains moisture variation or heavy impurities. Factory visits, operator feedback, installation records, and warranty terms can reveal details that product pages omit.
Small details count.
The comparison follows an evidence-based approach, using available technical documents, industry experience, customer reports, and manufacturer information. It also considers whether suppliers provide training, spare parts, software updates, and responsive service across different regions. No ranking is completely perfect. Market data changes, specifications may be presented differently, and some performance claims require independent verification. That uncertainty deserves attention, not concealment.
Readers can use this overview to compare suppliers more carefully and define their own priorities. A high-capacity sorter may suit a large export mill, while a simpler system could benefit a smaller processor with limited technical staff. The best choice depends on rice variety, contamination levels, line speed, budget, and local service access. Reliable decisions come from matching technology with operating reality.
How Rice Color Sorters Work and Why Ancoo Systems Matter
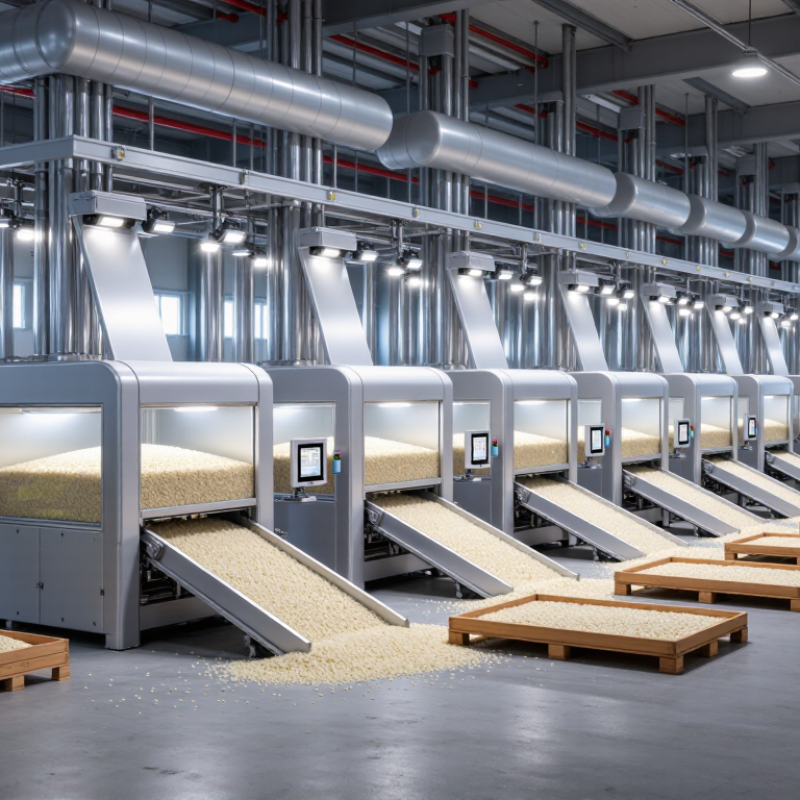
Rice color sorters use cameras, controlled lighting, and precise air jets to remove unwanted grains. Rice moves across narrow channels in a steady stream. Cameras inspect each grain within milliseconds. They detect differences in color, shape, size, and surface condition. Software compares each image with programmed quality settings. When a defect appears, a tiny air burst pushes that grain into a separate outlet.
This process helps remove yellow grains, stones, damaged kernels, and foreign particles. A clean lens matters. Dust can weaken image accuracy and increase unnecessary rejection. Operators must also check air pressure, feeder vibration, and lighting stability. In practical production, small adjustments often protect both quality and yield. A sorter that rejects too aggressively may waste good rice. A loose setting may allow defects to pass.
Reliable systems matter because rice quality changes from harvest to harvest. Strong equipment should handle different moisture levels, varieties, and processing speeds. Clear data records can help operators trace changes and improve settings over time. Yet no machine is flawless. Human inspection remains useful, especially when new defects appear. The best results come from combining accurate sensors, regular maintenance, trained operators, and honest performance checks. That combination supports cleaner output without treating automation as a complete replacement for judgment.
Criteria for Ranking the Top 10 Ancoo Manufacturers Worldwide
Ranking the top 10 Ancoo rice color sorter manufacturers requires more than comparing advertised speed. USDA’s Rice Outlook, October 2024, projected global milled rice production above 530 million metric tons. Such volume increases demand for stable, measurable sorting performance. Our ranking should examine detection accuracy, throughput, reject consistency, and product loss under real mill conditions. Independent test results matter more than showroom claims.
Experience also shows that reliability is practical, not decorative. We would assess camera resolution, lighting stability, air-valve response, software controls, and cleaning time. Energy use, spare-part availability, technician training, and warranty response deserve equal weight. ISO 9001 certification can support process control, but it cannot replace customer references. The FAO Food Outlook 2024 highlights continuing pressure on food systems and operating costs. Therefore, total ownership cost should include electricity, maintenance, downtime, and rejected good grains. No ranking is perfect. Data may be incomplete.
Tips: Request a witnessed test using your own rice samples. Measure broken grains, discolored kernels, and false rejects separately. Ask for twelve-month service records, not selected testimonials. Compare results across moisture levels and different varieties. A supplier with slightly lower capacity may deliver better yearly output when stoppages are fewer. Verify local technical support before signing. Small details often decide performance.
Profiles of the Leading Ancoo Rice Color Sorter Manufacturers
Leading rice color sorter manufacturers worldwide combine optical engineering, grain-processing experience, and practical field support. Their machines typically use high-resolution cameras, controlled LED lighting, and fast air ejectors to remove discolored or foreign grains. In a working mill, this means fewer broken kernels, steadier output, and cleaner bags. However, performance depends heavily on rice variety, moisture, and feed consistency.
Several manufacturers focus on high-throughput systems for large processing plants. Their profiles often show modular channels, touchscreen controls, automatic calibration, and remote diagnostic tools. Others serve smaller mills with compact machines that use less power and simplify daily maintenance. Details matter. A reliable supplier should provide test sorting with local rice samples, clear accuracy data, and replacement parts that arrive on time.
Experienced manufacturers also invest in service teams, operator training, and installation guidance. A technician should explain how to clean the camera window, adjust sensitivity, and inspect air pressure. These small actions protect sorting accuracy. Some published specifications can look impressive, yet real results may change under dusty conditions or uneven feeding. That is worth questioning. Buyers should compare usable capacity, reject rates, warranty coverage, and long-term support rather than choosing by price alone. A careful profile should mention both strengths and limitations, not only polished performance claims.
Comparison of Sorting Accuracy, Capacity, and Smart Features
A practical comparison of ten leading rice color sorter manufacturers should begin with measurable accuracy. The USDA Production, Supply and Distribution database places global milled rice output above 530 million metric tons in recent seasons. That scale increases demand for stable, high-throughput inspection. Top systems commonly advertise 99.9% or higher rejection accuracy. However, these figures often use clean test samples. Real mills face chalky grains, uneven moisture, dust, and mixed varieties. Independent trials matter more than brochures.
Capacity usually ranges from 4 to 12 metric tons per hour per channel, depending on grain quality and defect density. Larger models can process more rice, but excessive speed may reduce separation precision. A useful test should record good-grain loss, defective-grain removal, electricity use, and downtime. Small details matter. A blocked air nozzle can quietly damage results.
Smart features now include AI image recognition, multi-spectrum cameras, automatic sensitivity adjustment, remote alerts, and production reports. These tools reduce operator workload, yet connectivity does not guarantee better sorting. The FAO Rice Market Monitor emphasizes continuing quality pressures across global rice markets, but it does not validate individual machine claims. Buyers should request raw test data, sample conditions, and maintenance records. I would also examine performance after several hours of dust exposure. That test is less impressive, but more honest.
Top 10 Ancoo Rice Color Sorter Manufacturers Worldwide - Comparison of Sorting Accuracy, Capacity, and Smart Features
| Rank | Anonymous Manufacturer | Primary Rice Applications | Rated Capacity (t/h) | Typical Sorting Accuracy | Rejection Ratio | Camera Configuration | AI-Assisted Defect Recognition | Remote Monitoring | Air Consumption (L/min) | Overall Capability Score |
| 1 | Manufacturer A | White rice, parboiled rice, long-grain rice | 10–12 | 99.99% | 40:1–50:1 | Full-color RGB + infrared | Advanced | Yes | 900–1,100 | 9.6/10 |
| 2 | Manufacturer B | White rice, fragrant rice, broken rice | 8–12 | 99.98% | 35:1–45:1 | RGB + infrared | Advanced | Yes | 850–1,050 | 9.3/10 |
| 3 | Manufacturer C | White rice, brown rice, paddy rice | 8–10 | 99.98% | 35:1–45:1 | Full-color RGB + infrared | Advanced | Yes | 800–1,000 | 9.1/10 |
| 4 | Manufacturer D | White rice, glutinous rice, specialty rice | 6–10 | 99.97% | 30:1–40:1 | RGB + infrared | Advanced | Yes | 750–950 | 8.9/10 |
| 5 | Manufacturer E | White rice, parboiled rice, mixed grains | 6–8 | 99.97% | 30:1–40:1 | RGB color cameras | Standard | Yes | 700–900 | 8.6/10 |
| 6 | Manufacturer F | White rice, brown rice, medium-grain rice | 5–8 | 99.96% | 25:1–35:1 | RGB + infrared | Standard | Yes | 650–850 | 8.3/10 |
| 7 | Manufacturer G | White rice, broken rice, discolored grains | 5–7 | 99.95% | 25:1–35:1 | RGB color cameras | Standard | Yes | 600–800 | 8.0/10 |
| 8 | Manufacturer H | White rice, parboiled rice, low-grade rice | 4–6 | 99.95% | 20:1–30:1 | RGB color cameras | Standard | Optional | 550–750 | 7.7/10 |
| 9 | Manufacturer I | White rice, brown rice, specialty grains | 3–5 | 99.94% | 20:1–30:1 | RGB color cameras | Standard | Optional | 500–700 | 7.4/10 |
| 10 | Manufacturer J | White rice, broken rice, small-batch processing | 2–4 | 99.90% | 15:1–25:1 | RGB color cameras | Basic | Optional | 450–650 | 7.0/10 |
Note: Manufacturer names are intentionally anonymized. Capacity, accuracy, rejection ratio, and air-consumption figures are specification ranges that vary according to rice variety, moisture content, impurity load, feed consistency, and machine configuration. Final performance should be verified through a site-specific trial.
Global Applications, Service Networks, and Buyer Considerations
Choosing among the top ten rice color sorter manufacturers worldwide requires more than comparing machine prices. Each manufacturer should demonstrate practical experience with local rice varieties, moisture levels, and processing conditions. A reliable sorter should identify chalky grains, discolored kernels, stones, and foreign materials with stable accuracy. Ask for test results using your own rice samples, not only showroom demonstrations.
Global applications vary widely. Asian mills often need high-throughput sorting for long-grain and broken rice. African and Middle Eastern processors may prioritize dust resistance, simple controls, and flexible power systems. Service networks matter just as much as optical performance. Look for regional engineers, spare-parts warehouses, remote diagnostics, and clear response times. A strong supplier explains maintenance schedules in plain language. Vague promises deserve caution.
Tips: Request a sample trial, written accuracy data, operator training, and a three-year parts forecast. Check whether technicians can reach your facility quickly. Review energy use, air consumption, software updates, and cleaning access. Speaking with existing users can reveal delays that brochures hide. One overlooked detail is compressed-air quality; moisture can reduce sorting stability. Another is language support for operators. A technically advanced machine may still underperform when training is rushed. Even careful buyers can miss installation conditions, so leave room for reassessment after the first production season.